24/7 breakdown support across the Riverina0427 997 730[email protected]

Home / Services / Allen-Bradley PLC programming

SVC · Allen-Bradley

Allen-Bradley PLC programming, HMIs and migrations

Studio 5000 programming for ControlLogix, CompactLogix and GuardLogix, Rockwell HMIs, and staged migrations off SLC 500, PLC-5 and MicroLogix.

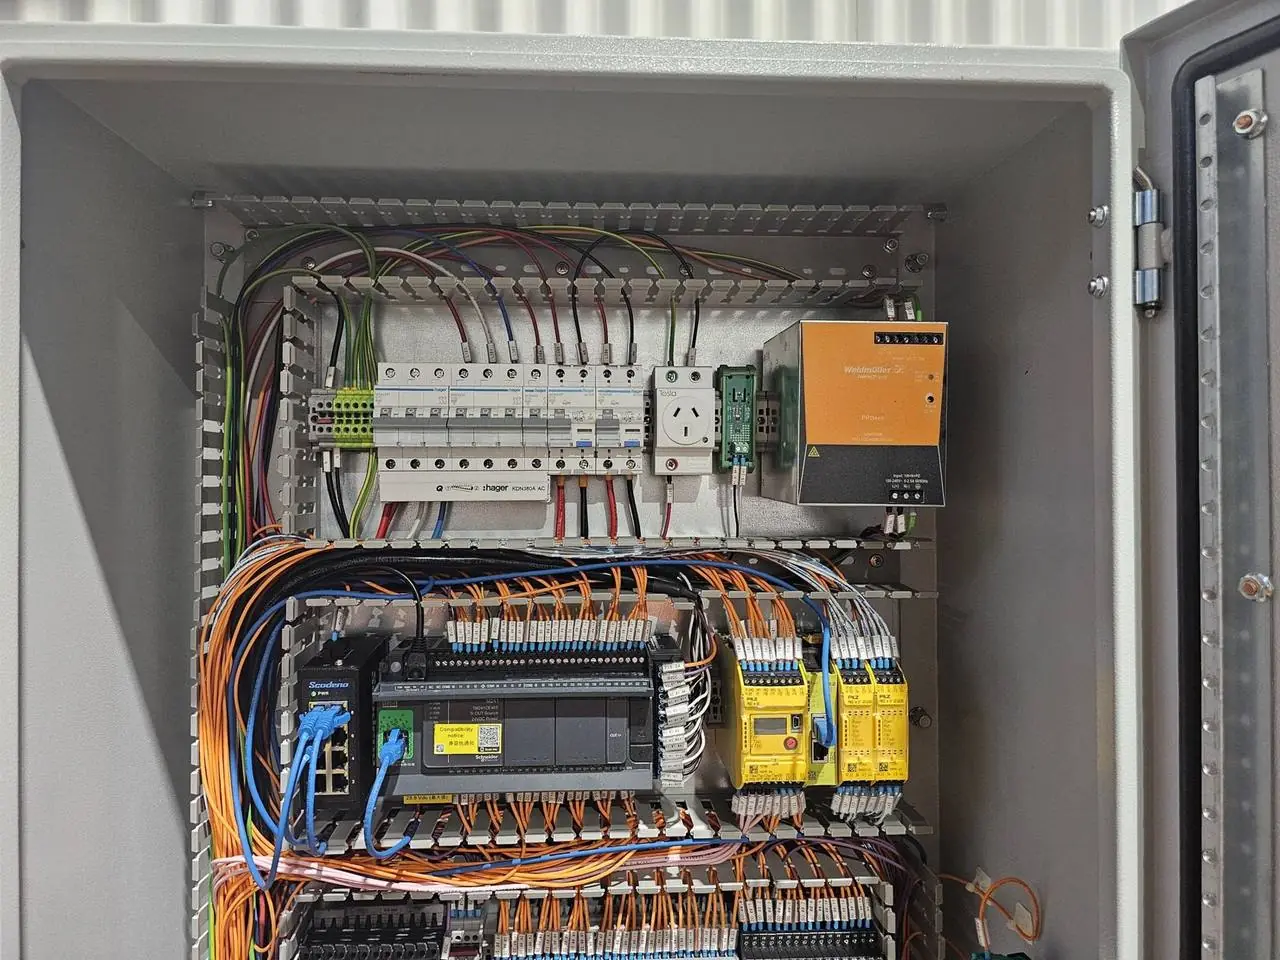
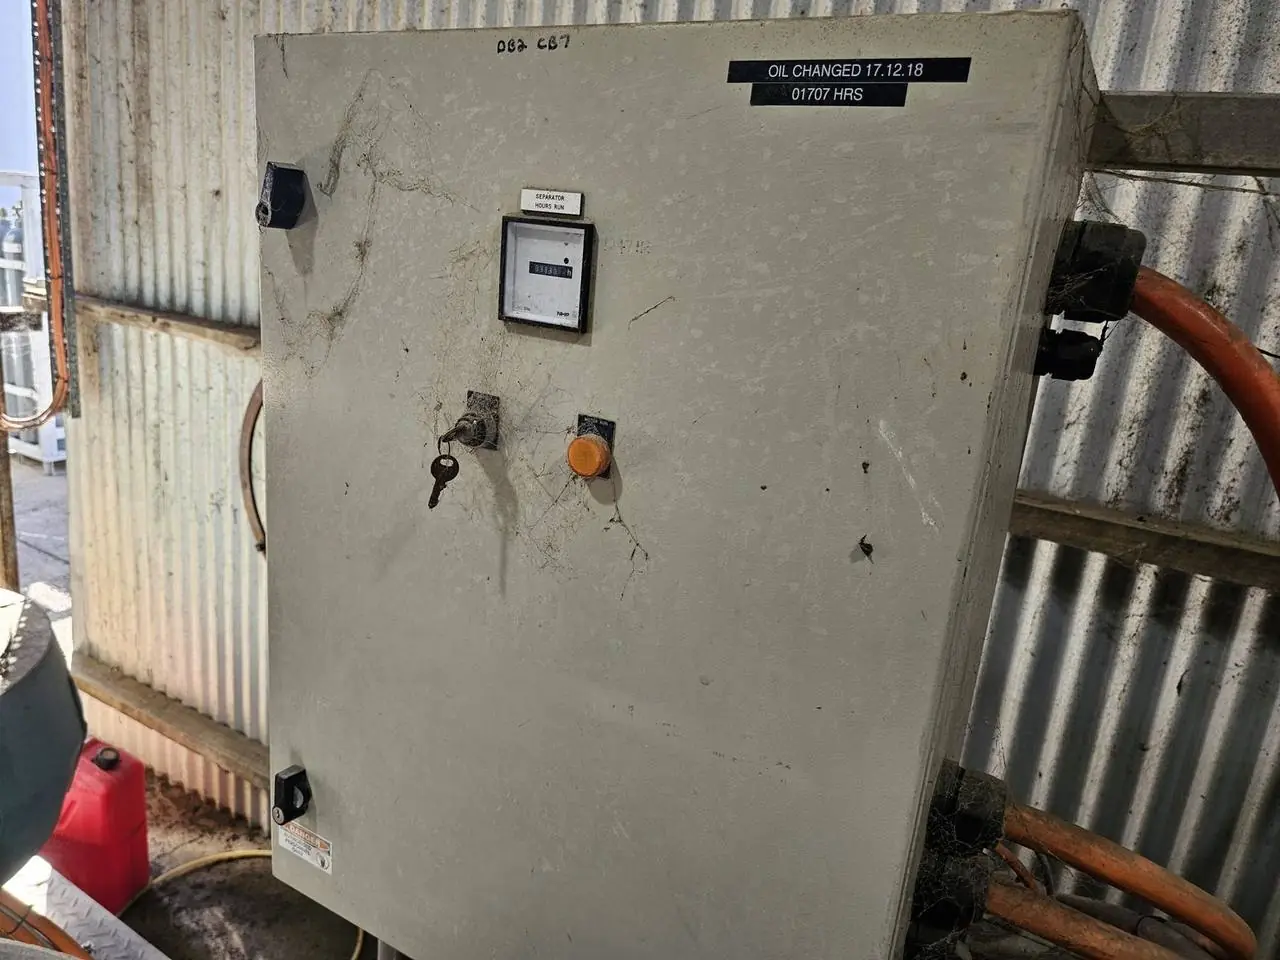
PLC control board with safety relays and terminal wiringOriginal legacy control panel before upgrade

SVC · Allen-Bradley · What we do

Rockwell control systems, written to be maintained.

Allen-Bradley is the most common PLC platform in Australian food, beverage and process plants. AMC programs new Logix systems, modifies and fault-finds existing ones, and replaces old SLC 500, PLC-5 and MicroLogix controllers before they fail and spares run out.

Our programs are structured, commented and checked against our in-house PLC and HMI software verification standard before they reach site, so your maintenance team can follow them. Because we also design and build the control panels, we can deliver a complete Rockwell system from drawings to commissioning, or work alongside your own engineers on an existing one.

What we do

  • ControlLogix and CompactLogix programming in Studio 5000
  • GuardLogix and Compact GuardLogix safety programming
  • PanelView Plus and FactoryTalk View ME/SE HMIs
  • SLC 500, PLC-5 and MicroLogix migrations to Logix
  • Modifications and fault finding on existing programs
  • Control panel design and build around Rockwell hardware
  • Staged cutovers to keep production running
  • Remote support where you allow secure access

Standards, platforms & tools

Studio 5000RSLogix 500RSLogix 5ControlLogixCompactLogixGuardLogixPanelView PlusFactoryTalk View

Migrating old Allen-Bradley PLCs

Off SLC 500 and PLC-5, without a long shutdown.

Rockwell has discontinued much of the SLC 500 and PLC-5 range. A planned migration costs far less than a breakdown with no spares. Read the SLC 500 and PLC-5 migration guide.

01

Audit what you have

Back up and review the existing program, I/O, networks and HMIs, and identify what is undocumented.

02

Plan the cutover

Decide what can be converted, what should be rewritten and how to stage it around production.

03

Convert and improve

Move the logic to Studio 5000, clean up structure and alarms, and fix known problems while we're in there.

04

Test before site

Test the new program and HMI in the workshop before anything touches your plant.

05

Cut over in stages

Swap hardware and software in planned windows, often weekends or shutdowns.

06

Hand over properly

As-built drawings, commented programs, backups and training. See our PLC upgrade guide.

How we work

One team for panel, program and commissioning.

Most PLC problems come from the gaps between the panel builder, the programmer and the commissioning engineer. We do all three, so the I/O list, the drawings and the program agree, and someone who wrote the code is on site when it goes live.

We work Australia-wide. Programming and testing happen in our Griffith workshop, then we commission on site and support you remotely afterwards where your security policy allows.

  • Program and I/O review
  • Functional description
  • Programming to our standard
  • Workshop testing
  • Commissioning on site
  • Backups, drawings and training

Proof

See it on the job.

Related projects include legacy control system upgrades, an automated CIP and filler control system with a validated safety system, and a pallet wrapper safety system.

Where we work

Griffith-based. Riverina and Australia-wide.

We program Allen-Bradley systems for sites across the Riverina and Australia-wide.

GriffithLeetonYendaHanwoodYoogaliNarranderaDarlington PointColeamballyHayHillstonWagga WaggaMildura

FAQs

Common questions

Which Allen-Bradley PLCs do you work on?

ControlLogix, CompactLogix, GuardLogix and Compact GuardLogix in Studio 5000, plus legacy SLC 500, PLC-5 and MicroLogix in RSLogix 500 and RSLogix 5.

Can you migrate an SLC 500 or PLC-5 to CompactLogix or ControlLogix?

Yes. We audit the existing system, convert and improve the logic, test it in our workshop and cut over in planned stages to keep downtime short. See our SLC 500 and PLC-5 migration guide and MicroLogix replacement options.

Do you do Rockwell HMIs?

Yes. PanelView Plus and FactoryTalk View ME and SE screens, including alarm handling and trends. Replacing an old screen? See PanelView HMI replacement.

Can you program GuardLogix safety controllers?

Yes. We program GuardLogix and Compact GuardLogix safety systems as part of AS 4024 machine safety projects. See machine safety.

Can you work on a program someone else wrote?

Yes. We fault-find and modify existing programs, and document what we change.

Do you work outside the Riverina?

Yes. We deliver Allen-Bradley work Australia-wide, with workshop testing in Griffith, on-site commissioning and remote support.

Next step

Got a plant, machine or board that needs sorting?

Send us the scope, drawings or a few photos. An engineer reads every request and comes back within one business day with next steps and a clear, upfront price.

Project engineer or OEM? Send a P&ID, equipment list or scope for a budget price.

Call nowEmailGet a quote